
Predictive maintenance from fuel data at a pumping station
How fuel monitoring on diesel water pumps in Sierra Leone stopped theft — and then caught a 15% consumption jump caused by clogged filters.
A plant that lives on river water
A manufacturing company’s plant in Sierra Leone needs huge volumes of water to cool its equipment. Its pumping stations on the banks of a nearby river take water and pump it to tanks on site; uninterrupted pumping is what keeps the plant running. The stations use industrial water pumps driven by 300 kW diesel engines.
Theft first — diagnostics second
The company wanted to monitor fuel consumption and engine run time, stop fuel theft and misuse, and use fuel data for engine diagnostics.
Level and flow on a single wire
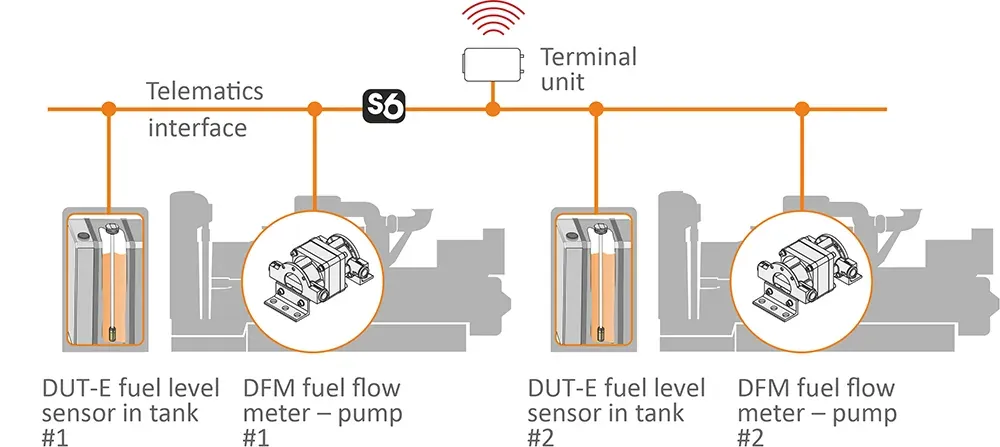
A DUT-E CAN fuel level sensor sits in each pump’s feed tank, and a DFM D CAN differential flow meter in the supply and return lines measures consumption directly. Together they provide more than 50 fuel parameters over CAN J1939 — level, volume and temperature in the tank, total consumption, flow and temperature in each line, and run time and fuel use in idle and normal modes.
All units, including the data logger, are connected over a single S6 cable, which cuts installation effort and wiring mistakes.
Theft was solved quickly: level sensors flag drains from the tank instantly, and the flow meter leaves no way to take diesel from the lines. Then the flow data showed supply and return flow falling for no obvious reason while real consumption jumped by 15% — about $2,620 extra per pump per week. Inspection found clogged fine filters, caused by unstable fuel quality. An automatic alarm now warns when flow drops below a threshold, maintenance schedules were optimised, and the plant saves on fuel, repairs and sudden breakdowns.
Task → Solution → Result
Theft and blind maintenance
Diesel water pumps critical to the plant, with fuel theft and no engine diagnostics.
DFM D CAN + DUT-E CAN on S6
Over 50 fuel parameters from tank and fuel lines on one wire.
+15% jump caught
Theft stopped; clogged filters found from flow data; filter alarms and optimised maintenance.
Want product info and guidance from our experts?
Tell us about your fleet and we'll recommend the right measurement setup.